
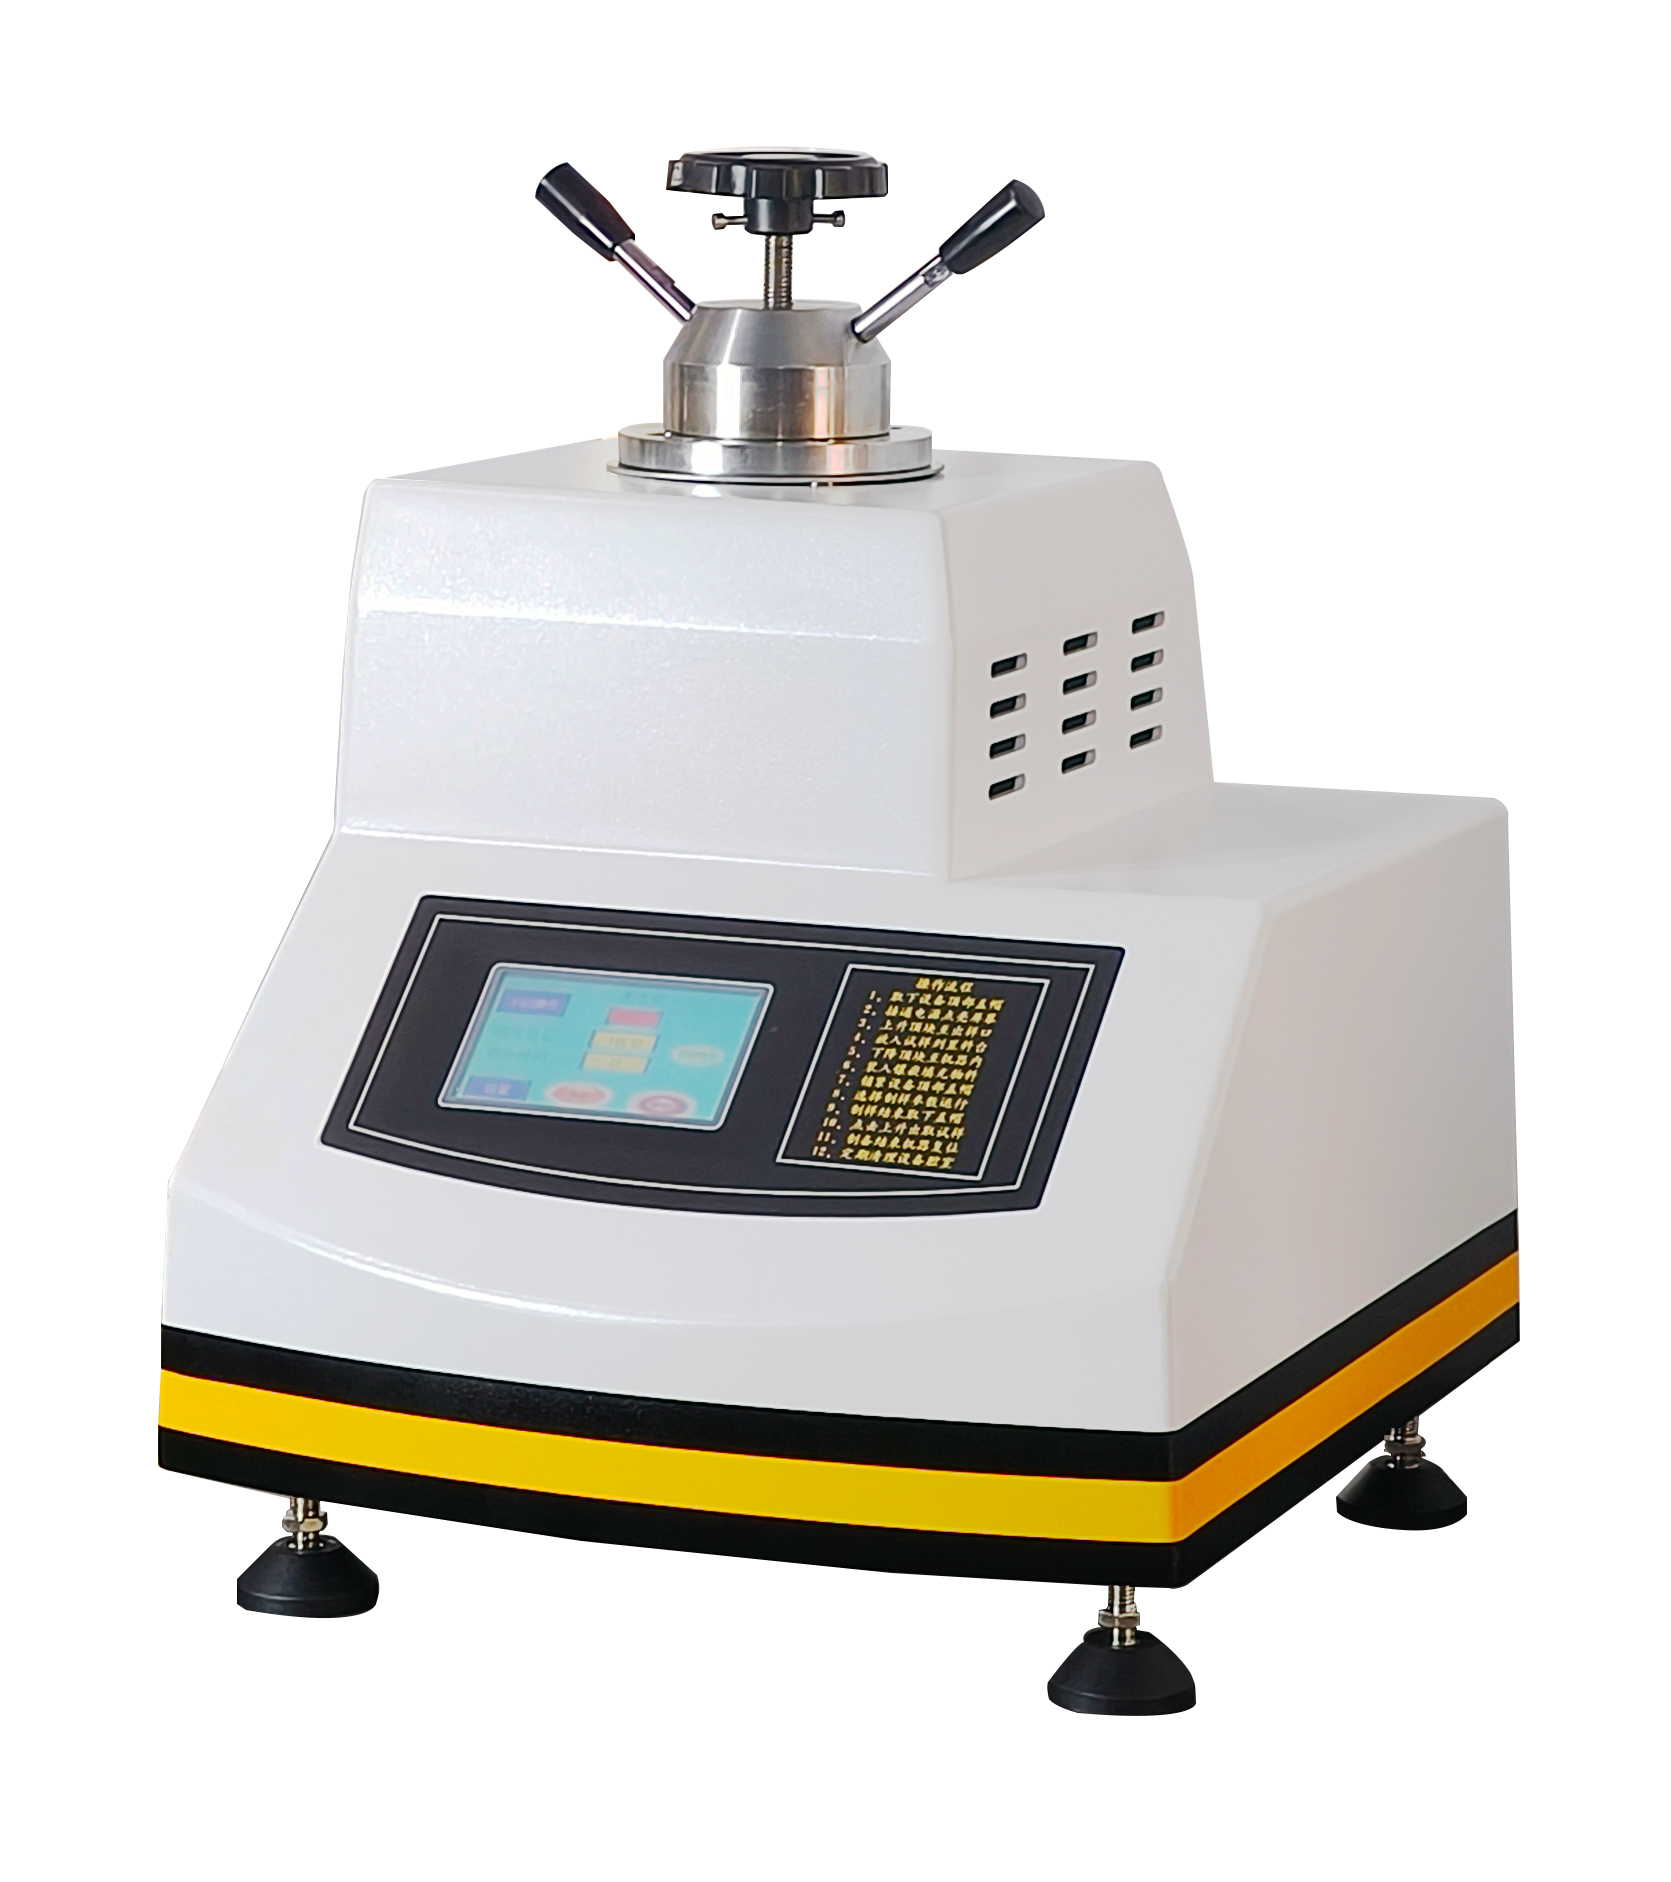
Automatic Mounting Presses
ZXQ-5A Automatic Metallographic Mounting Press
Automatic Mounting Press
Model ZXQ-5A
Details
Intelligent automatic, automatic and manual mounting with heating and water cooling, ¢25–45 mm interchangeable dies
Automatic Mounting Press
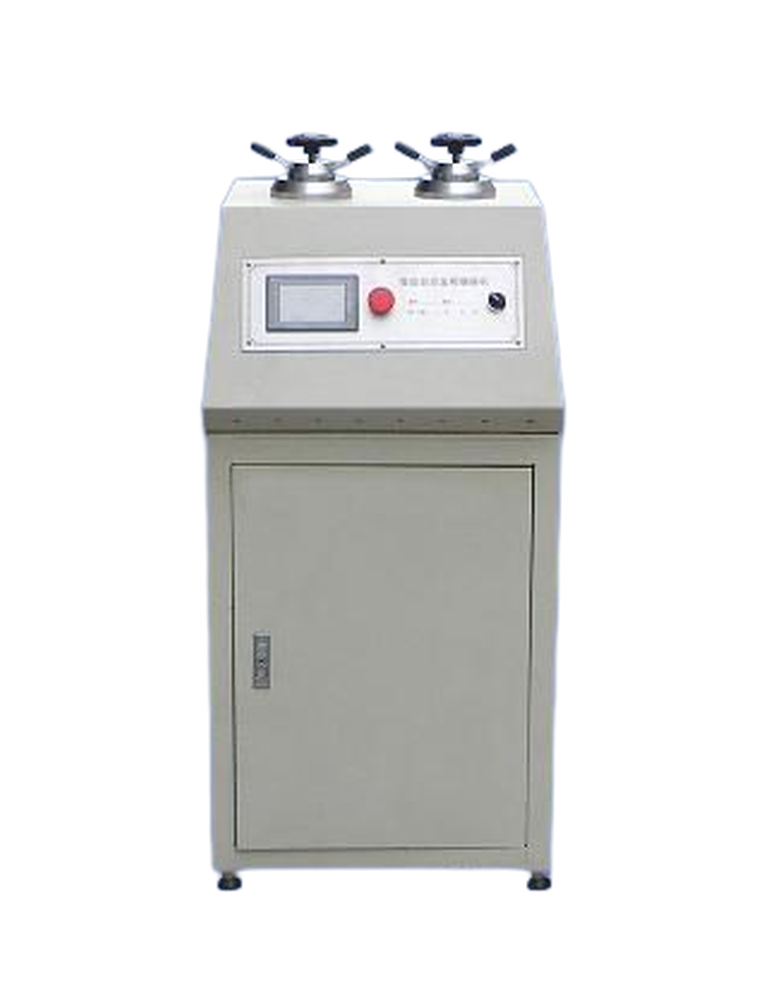
Automatic Mounting Press
Mounting encapsulates small, irregular or edge-critical specimens in resin so later grinding has a flat support and the edge does not round over. Hot mounting cures thermosetting resin at 150–180 °C and 20–30 MPa for 5–15 min, then demoulds after cooling; cold mounting uses epoxy or acrylic at room temperature for heat-sensitive materials. The ZHONGYAN ZXQ series integrates heating, pressing and water cooling, one or two specimens per cycle, with interchangeable Ø25–45 mm dies.
The preparation/inspection workflow built around the Metallographic Mounting Presses — every step has its own consumables and parameters.
| Die sizes | Ø 25 / 30 / 40 / 45 mm |
|---|---|
| Heating range | 0 – 200 °C |
| Pressing force | 0 – 30 MPa |
| Specimens per cycle | 1 – 2 |
| Cooling | Built-in water circuit |
Many specimens needing consistency → intelligent automatic press with programmed temperature and pressure.
Heat-sensitive aluminium alloys, quenched foils or coatings → cold mounting with epoxy, curing at room temperature without altering the structure.
Conductive mounting for SEM/EBSD → use conductive resin with carbon or metal filler, or carbon-coat after mounting.
下面三栏分别是同行业工件的真实处理方式、对应的检测方法,以及现场最常要算的几个量。
Lines are staffed 08:30–17:30 on business days. Leave a message after hours and we reply the next working day.
Call Us021-51693591 Email for a quotezhongyanyiqi@163.com Send a messageInclude material and specimen size for a faster answerShortlisted from our own range only; final specifications confirmed by our engineers. Full selection →